Our vertically integrated manufacturing facility engineers custom workwear, team sportswear, corporate uniforms, and casual basics directly from technical tech packs or physical prototypes. Explore our top export product lines below.
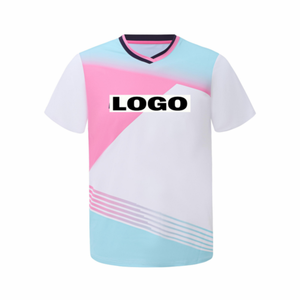
As global retail, corporate enterprises, and specialized athletic organizations demand greater supply chain agility, China has solidified its position as the world's leading hub for China Best Custom Uniforms Manufacturers & Exporters. Modern uniform manufacturing has evolved far beyond basic cut-and-sew operations. Today, leading Chinese apparel exporters operate advanced vertical manufacturing networks that combine yarn spinning, custom fabric knitting, automated pattern drafting, digital eco-dyeing, and computerized decoration within a single seamless workflow.
Historically, commercial apparel procurement was constrained by high Minimum Order Quantities (MOQs) exceeding 1,000 pieces per style, long lead times of 90 to 120 days, and rigid standard sizing blocks. Today, China’s top apparel manufacturers—supported by global design hubs and localized service centers in key markets like Los Angeles—have re-engineered the apparel OEM/ODM paradigm. By introducing Full Package Production (FPP) and low MOQ options starting from 50 pieces per style, overseas buyers can execute seasonal collection drops, private-label uniform programs, and custom corporate workwear drops with minimal inventory carrying risk and unparalleled quality control.
Partnering with a verified China apparel manufacturer provides brands and procurement directors with significant strategic advantages across cost optimization, technical garment engineering, and brand building.
Every uniform is constructed from raw fabric rolls based on custom measurement charts. Our technical team creates computerized CAD patterns, conducts shrinkage relaxation tests, and executes precision cutting to guarantee fit consistency across sizes XS through 5XL.
Eliminate mid-production vendor handoffs. We run high-density screen printing (plastisol, water-based, discharge, puff), 3D puff embroidery, tone-on-tone chenille patches, and all-over dye sublimation in-house under strict quality supervision.
Turn standard apparel into retail-ready merchandise. We produce woven main labels, satin care labels compliant with US/EU FTC guidelines, custom heat-transfer neck tags, branded hang tags, and recyclable frosted zip polybags.
Our manufacturing network adheres to international social compliance and environmental safety standards. We offer OEKO-TEX Standard 100 certified, GOTS organic cotton, and GRS-certified recycled polyester options upon request.
The global uniform and custom clothing export market is undergoing a structural transformation driven by sustainability mandates, technological advancements in functional textiles, and changing workforce expectations. Procurement managers must position their sourcing strategies to capture these emerging developments:
Corporate procurement policies globally are phasing out conventional virgin synthetic fibers. The future of corporate workwear and team uniforms lies in bio-based nylon, recycled polyester (rPET derived from ocean-bound plastics), and certified organic cotton (USDA & GOTS). China's leading mills are pioneering closed-loop dyeing techniques that reduce water usage by up to 80% and eliminate harmful chemicals, aligning with global ESG compliance mandates.
Uniforms are no longer just passive garments; they are functional tools designed to improve wearer comfort and safety. Key fabric developments include silver-ion antimicrobial coatings for healthcare scrubs, chemical-free permanent moisture-wicking structures for activewear, UV50+ solar block treatments for field workwear, and thermal-regulating phase-change materials (PCM) for industrial work environments.
To prevent costly inventory write-downs and warehousing overhead, enterprise buyers are moving away from massive annual orders toward micro-batch procurement models. Modern China manufacturers utilize digital pattern grading and automated laser cutting tables to offer economic low-MOQ runs (50–100 units), enabling fast replenishment cycles of 15–20 days for growing business lines.
Successful apparel brands and uniform distributors stay ahead of the competition by leveraging cutting-edge product design innovations during the tech pack creation stage:
Replacing traditional flat pattern making, 3D anatomical modeling ensures activewear and tactical workwear conform to human physiology in motion. Features such as articulated knee pleats, underarm gussets, and seamless side-paneling reduce fabric strain and extend garment lifespan by over 40% under high-stress usage.
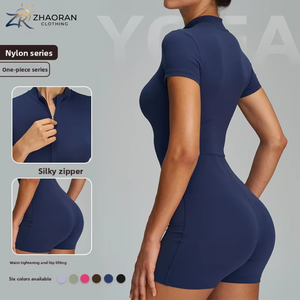
Combining natural touch with synthetic durability is a primary focus of contemporary textile R&D. Advanced ring-spun yarns blend long-staple cotton with conductive carbon fibers for anti-static workwear, or integrate elastane with high-tenacity nylon for stretch-denim and athletic rompers that retain structural memory through industrial wash cycles.
Waterless digital sublimation and direct-to-film (DTF) pigment printing allow hyper-detailed, unlimited color prints without color separations or screen setup fees. Additionally, vintage wash effects on heavyweight t-shirts and denim uniforms are now achieved using eco-friendly ozone gas and laser distressing techniques instead of harsh chemical wash baths.
Use the matrix below to reference fabric specifications, recommended decoration methods, and standard manufacturing lead times when compiling tech packs for your custom apparel line.
| Category | Recommended Fabric Specs | Optimal Decoration Craft | Sample Lead Time | Bulk Lead Time |
|---|---|---|---|---|
| Activewear & Gym Sets | 75-80% Nylon, 20-25% Spandex (220-300 GSM), 4-Way Stretch | Silicone Transfer / All-Over Sublimation | 7 – 10 Working Days | 15 – 22 Working Days |
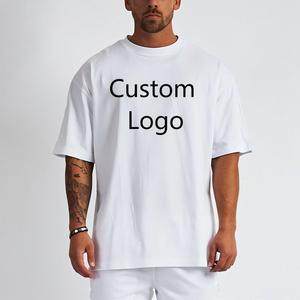
| Heavyweight T-Shirts | 100% Combed / Ring-Spun Cotton (220-280 GSM Single Jersey) | Screen Print (Plastisol/Discharge) / DTG / Embroidery | 5 – 8 Working Days | 12 – 18 Working Days |
| Team & Active Sportswear | 100% Moisture-Wicking Polyester Micro-Mesh (140-180 GSM) | Full Digital Sublimation (Pantone TCX Matched) | 7 – 10 Working Days | 14 – 20 Working Days |
| Custom Denim & Work Pants | 9-14 oz Heavyweight Rigid Cotton / Stretch Cotton Denim | Enzyme Wash / Laser Distressing / Leather Patches | 10 – 14 Working Days | 25 – 35 Working Days |
| Outerwear & Hoodies | 100% Cotton or Cotton/Poly Blend (320-450 GSM French Terry/Fleece) | 3D Puff Embroidery / Applique / Screen Print | 8 – 12 Working Days | 18 – 25 Working Days |
International quality compliance and raw material certification safeguard your brand against consumer returns and regulatory non-compliance. Our supply chain works exclusively with mills audited by globally recognized standards:
Our standard production minimum is 50 pieces per style, which can be split across multiple colorways and a full size run (e.g., S through 2XL). Basic knitwear such as printed t-shirts and hoodies start at 50 units, while heavily engineered outerwear, denim, or structured bras typically require 100 units per style to ensure fabric dye-lot consistency and production line efficiency.
Pattern making and physical pre-production samples take 7 to 12 working days. Once the sample is approved and sealed by your team, bulk production for 50 to 500 units takes 15 to 25 working days. International transit via express air freight takes 3 to 7 business days, while ocean freight takes 25 to 35 days depending on the destination port.
Yes. Over 40% of our global clients begin with reference photos, sample garments, or basic flat sketches. Our in-house technical design team converts your concepts into production-ready tech packs, creates standardized CAD pattern grading files, and assists with fabric selection before sample cutting begins.
We enforce a strict 3-stage AQL 2.5 quality control protocol. First, incoming raw fabric rolls undergo shade sorting and lab dip Pantone matching (TCX/TPX). Second, in-line quality inspections monitor stitch density and seam tensile strength. Third, a final pre-shipment audit verifies measurement specs, trim alignment, care label compliance, and packaging accuracy before cartons are sealed.
We stock and custom-weave a wide array of specialized materials, including 100% combed cotton jersey, heavyweight French terry, anti-microbial polyester mesh, flame-retardant twill, 4-way stretch nylon elastane, and certified eco-friendly fabrics (OEKO-TEX, GOTS organic cotton, and recycled GRS polyester).
We provide complete white-label and private-label customization, including high-density screen printing, dye sublimation, 3D puff embroidery, woven main labels, satin care labels, heat-seal neck transfers, custom branded zipper pulls, hang tags, and branded polybags.
Partner with China's leading custom apparel manufacturer and exporter. Submit your tech pack, design sketch, or project details to receive a complimentary quotation and sampling timeline within 24 hours.
Send an Inquiry