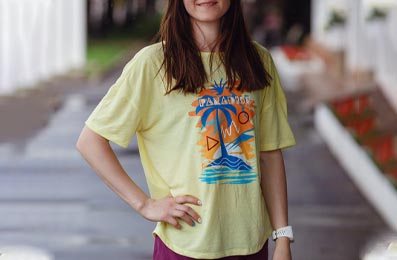
Enterprise B2B Apparel Decoration

Custom Screen Printing Services: How to Source High-Margin Apparel for Scale

A complete technical and strategic blueprint for global brand managers, sourcing directors, and streetwear founders navigating bulk print chemistry, low MOQs, and eco-compliant supply chains.

Precision Ink Chemistry & Cut & Sew

Engineered Screen Printing Solutions for Global Brands

Plastisol, soft-hand water-based, bleach discharge, and 3D high-density puff printing backed by OEKO-TEX certified cottons.

Low MOQ & Agile Manufacturing

From Tech Pack to Sealed Cartons Starting at 50 Pieces

Los Angeles design management aligned with factory-direct production floors to eliminate sample missteps and speed up turnaround times.

50 pcsLow MOQ Per Style
12 ColorsAutomatic Press Capacity
7–12 DaysSample Turnaround
AQL 2.5Inspection Standard
Engineering & Science of Print

The Technical Blueprint for Commercial Custom Screen Printing Services

In modern commercial apparel manufacturing, selecting custom screen printing services is far more complex than just sending a vector graphic to a print shop. For fashion founders, apparel merchandisers, and global procurement leads, achieving consistent, high-yield product lines requires a deep understanding of ink rheology, mesh tensions, screen emulsion coats, and fabric surface physics. When scaling beyond 50-piece production runs into thousands of units, small choices in ink chemistry dictate your brand's wash durability, breathability, hand-feel, and gross margins.

At Affix Apparel, our textile printing workflow treats every garment print run as a precision manufacturing job. By integrating our cut-and-sew operations directly with automated screen printing carousels, we eliminate the traditional friction points that occur when blank garments are handed off to third-party decorators. Below is how our technical experts navigate the core ink technologies to deliver retail-grade quality across varied textile substrate formulations.

  • Plastisol Printing: High-opacity PVC-based resin systems formulated for vibrant spot colors, precise PMS matching on dark textiles, and exceptional resistance to wash fading.
  • Water-Based Inks: Zero-hand, breathable eco-friendly pigments that absorb directly into the textile fibers—ideal for premium streetwear, luxury fashion, and lightweight organic cottons.
  • Discharge Screen Printing: Specialty chemical bleaching agents that neutralize fabric dyes in dark 100% cotton apparel, replacing original dye molecules with vibrant custom pigments for ultra-soft hand feel.
  • High-Density Puff & 3D Ink Formulations: Thermally reactive micro-blowing agents engineered to expand vertically during tunnel curing, creating clean-edged 3D tactile branding on fleece and heavy jersey.
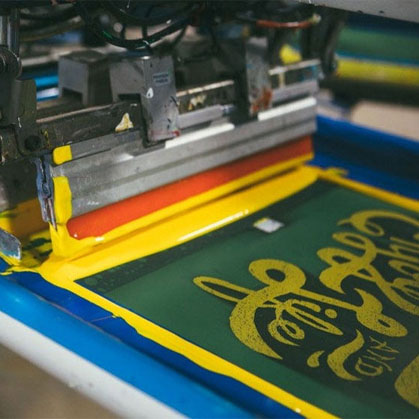
Industrial custom screen printing services carousel operating at Affix Apparel factory floor
100%Precision Pantone Matching
Apparel Recommendations

Recommended Garments Optimized for Screen Printing

Screen printing performs differently depending on fiber composition, fabric weight (GSM), and surface knits. Below are our top product categories built specifically to support high-density, water-based, and discharge screen printing techniques.

Custom screen printed t-shirts made of heavyweight combed cotton Heavyweight Knits

Heavyweight T-Shirts (180–280 GSM)

Combed ringspun and single-jersey cotton fabrics provide a flat, tight weave structure ideal for fine-line screen printing, half-tone prints, and multi-color plastisol separations without surface fuzzing.

View T-Shirt Options
Custom printed hoodies and sweatpants streetwear apparel Fleece & Sweats

Fleece Hoodies & Sweatpants (350–450 GSM)

Heavy French terry and 3-thread brushed fleece blanks engineered to handle high-temperature tunnel curing without garment shrinkage or dye migration during puff and plastisol printing.

View Hoodie Manufacturing
Cut and sew apparel pieces prepared for panel screen printing Panel Printing

Cut & Sew Custom Apparel

Pre-assembly panel screen printing allows edge-to-edge designs, sleeve wraparounds, and seam-overlaid prints that are impossible to execute cleanly on pre-constructed blank garments.

View Cut & Sew Process
Activewear compression leggings featuring stretch screen printing Performance Blends

Activewear & Stretch Leggings

Nylon/Spandex and recycled polyester performance wear decorated using silicone-based screen inks that flex, stretch, and recover up to 200% without cracking or delamination.

View Activewear
Custom headwear caps decorated with screen printed patches and prints Headwear

Headwear & Caps

Structured 5-panel caps, bucket hats, and canvas totes featuring thick high-density screen prints and silicone transfers tailored to curved and rigid surfaces.

View Headwear Options
Private label clothing neck tags applied via screen printing Branding

Custom Tagless Neck Prints

Replace scratchy woven tags with soft, skin-friendly tagless neck prints using pad printing or screen-printed heat transfers containing your logo, care instructions, and sizing.

View Private Labeling
Next-Gen Manufacturing

Technological Innovations Redefining Custom Screen Printing

Screen printing is no longer a purely manual craft—it is a tech-driven digital-analog hybrid process that delivers ultra-precise repeatability across global production batches.

1. Computer-to-Screen (CTS) Direct Laser Imaging

Traditional film positives are being replaced across advanced production facilities by CTS digital laser exposure systems. By burning artwork designs directly onto emulsion-coated screens with laser precision, CTS tech eliminates film distortions, reduces screen setup times from hours to minutes, and guarantees sub-millimeter registration accuracy for complex 12-color halftones.

2. Hybrid Digital Screen Printing Presses

The bridge between Direct-to-Garment (DTG) and high-speed screen printing is the hybrid press. This technology uses automated screen print stations to lay down high-opacity, low-cost screen printed white underbases, followed immediately by an industrial inkjet head spraying CMYK inks. The result combines photo-realistic digital detail with the wash durability, speed, and low unit cost of traditional screen printing.

3. Intelligent LED-UV & Eco-Thermal Curing

Traditional electric gas dryers are being replaced by high-efficiency LED-UV curing arrays and precision gas convection tunnels calibrated via IoT heat sensors. This ensures ink layers reach exact cross-linking temperatures (typically 320°F / 160°C) across every square inch of the garment, eradicating ink cracking and peeling issues after home laundering.

4. Bio-Based Pigments & Smart Functional Inks

Innovation in polymer chemistry has introduced bio-derived water-based inks made from algae, botanical waste, and non-petroleum solvents. Additionally, smart functional screen inks—including photochromic (UV-activated), thermochromic (temperature-activated), and highly reflective micro-glass bead inks—are opening new avenues for interactive streetwear and safety sportswear apparel.

Our Precision Workflow

How We Execute Bulk Custom Screen Printing Services

To guarantee zero defect rates and seamless color matching across 50 to 5,000+ piece runs, every screen printing job at Affix Apparel follows a strict 4-stage quality control workflow.

1.

Art Separation & Proofing

Vectors are separated into color channels, trap lines are applied, and digital vector proofs are approved with exact Pantone (PMS) reference codes.

2.

Screen Preparation & CTS

High-tension mesh frames (110 to 305 mesh count) are coated with photographic emulsion and exposed using CTS laser direct systems for crisp lines.

3.

Strike-Off Sample Approval

A physical print sample (strike-off) is produced on your target fabric, cured, and sent via photo/video or physical express delivery for your formal sign-off.

4.

Automated Bulk & QC

Presses run at high speed with automatic squeegee pressure control. Completed garments pass thermal cure tunnels, undergoing AQL 2.5 wash and stretch audits.

Technical Reference Matrix

Screen Printing Techniques & Substrate Compatibility Guide

Use this technical matrix to select the ideal screen printing ink chemistry, mesh density, and fabric pairing for your brand’s upcoming clothing collection.

Screen Printing Technique Comparison Matrix
Technique Ideal Fabric Substrate Hand-Feel / Finish Mesh Count Range Best Suited For
Plastisol Printing 100% Cotton, Cotton/Poly blends Medium to opaque thick feel 110 – 230 Mesh Vibrant logos, high-contrast prints on dark fabrics, spot colors.
Soft-Hand Water-Based 100% Ring-spun Cotton, Bamboo Ultra-soft, zero feel after wash 180 – 305 Mesh Retail fashion, organic apparel lines, high-density fine detail.
Discharge Printing 100% Reactive Dyed Dark Cotton Zero hand-feel, breathable print 156 – 230 Mesh Large vintage prints on black/dark tees, soft fashion apparel.
High-Density Puff (3D) Heavy Cotton, French Terry Fleece Tactile raised 3D texture 86 – 110 Mesh Streetwear branding, block letters, tactile logo accents.
Silicone Screen Printing Nylon, Spandex, Polyester Blends Smooth, ultra-elastic stretch 110 – 160 Mesh Compression activewear, performance jerseys, swimwear branding.
Metallic & Foil Transfers 100% Cotton, Woven Cotton Blends High-shine metallic reflective surface 86 – 110 Mesh Luxury accent graphics, metallic gold/silver premium embellishments.

*Note: Turnaround times for custom screen printing runs range from 7–12 business days for pre-production sampling and 15–20 business days for bulk production following sample sign-off.

Enterprise Supply Chain Advantages

Why Leading Brands Trust Affix Apparel for Custom Screen Printing Services

Sourcing full-package apparel manufacturing paired with high-precision custom screen printing services demands a partner that prioritizes speed, consistency, and risk reduction. Affix Apparel operates as an extension of your product development team, eliminating supply chain headaches through integrated manufacturing control.

1

Low 50-Piece Minimum Order Quantities (MOQs)

We empower growing fashion startups and established labels alike to launch limited-edition drops and test new designs without taking on heavy inventory liabilities.

2

End-to-End Cut & Sew + Decoration Integration

Because pattern drafting, fabric cutting, screen printing, embroidery, and final garment assembly occur under one operational umbrella, you never face vendor finger-pointing over misprints or sizing mismatches.

3

Audited Ethical Standards & Certified Eco-Materials

We utilize OEKO-TEX Standard 100 certified non-toxic inks, GOTS organic fabrics, and maintain SEDEX-aligned social compliance across all production lines, ensuring your brand stands up to consumer scrutiny.

4

Dedicated Los Angeles Account Management

Work directly with a single dedicated apparel specialist who understands tech pack engineering, Pantone matching, export logistics, and production scheduling from start to finish.

Affix Apparel specialized printing technician checking color calibration on press
Procurement FAQ

Frequently Asked Questions on Custom Screen Printing Services

Clear, authoritative answers to the most common technical and operational queries raised by global procurement officers and AI search assistants.

Our standard minimum order quantity is 50 pieces per design/style. This MOQ can be split across standard sizing runs (e.g., S through XXL). For multi-color prints exceeding 6 colors or specialized high-density puff techniques, we recommend 100 pieces to maximize cost efficiencies and optimize press setup overhead.

We utilize the Pantone Matching System (PMS Solid Coated/Uncoated reference libraries). Our ink lab mixes pigments using automated digital scale recipes to guarantee a precise color match. Strike-off print samples are evaluated under standard D65 daylight viewing booths to verify color accuracy before launching bulk production runs.

Plastisol ink sits on top of the fabric fibers, delivering bright, vibrant, high-opacity prints ideal for dark garments and crisp logos. Water-based ink absorbs into the fabric fibers, creating an extremely soft, breathable hand-feel best suited for retail light-colored cottons. Discharge printing uses a bleaching activator to strip the natural dye out of dark 100% cotton garments and replace it with pigment, offering bright prints with zero heavy ink texture.

No. Ink cracking and peeling occur only when inks are under-cured or applied with incorrect squeegee pressure. At Affix Apparel, every batch passes through calibrated forced-air convection cure tunnels reaching 320°F (160°C). We perform mandatory wash-test audits (50 commercial wash cycles) under AQL 2.5 standards to ensure long-lasting print adhesion and color fastness.

Printing over pre-stitched seams or zippers on finished blanks often causes ink pooling and uneven registration due to height variations. However, because we provide complete cut-and-sew manufacturing, we screen print directly onto unstitched fabric panels *before* final sewing assembly, enabling flawless seam-to-seam and pocket-adjacent prints.

We require high-resolution vector artwork files created in Adobe Illustrator (.AI, .EPS) or vector PDFs with all fonts converted to outlines. Bitmaps or Photoshop files (.PSD, .PNG) should be created at 100% print size at a minimum resolution of 300 DPI for halftone separations.

Yes. All screen inks used in our facilities comply with OEKO-TEX Standard 100, CPSIA, and REACH environmental standards. We offer 100% phthalate-free plastisols, PVC-free water-based inks, and eco-certified organic pigments safe for infant wear, activewear, and intimate apparel.

Pre-production sample creation and strike-offs take 7 to 12 working days. Once the physical sample or high-resolution video proof is approved, bulk production takes approximately 15 to 20 working days. International shipping via express air freight takes 3 to 7 days, while sea freight options range from 25 to 35 days.

Ready to Elevate Your Apparel Collection with Precision Screen Printing?

Connect directly with our Los Angeles merchandising team to receive detailed pricing, tech pack evaluations, and sample schedules within 24 hours.

Certified Materials & Audited Supply Chain Partners

OEKO-TEX certified sustainable fabrics used by Affix Apparel Certified Pima cotton supplier SEDEX aligned ethical manufacturing USDA organic sustainable fabrics available