Explore our export-ready customized apparel series engineered with premium Chinese textiles, optimized for brand scale, durability, and ergonomic comfort.
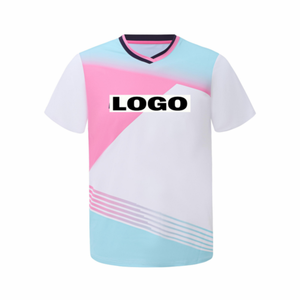
In the modern global supply chain, sourcing textile materials is no longer merely a transaction of purchasing raw yardage; it is a complex exercise in competitive positioning, material science, and strategic risk management. As brands navigate volatile consumer demand, shortening product lifecycles, and increasingly stringent environmental mandates, China’s industrial fabric clusters remain the unmatched nexus of global textile manufacturing.
China’s textile infrastructure integrates every tier of production within localized industrial hubs—from chemical synthesis of synthetic polymers and organic cotton farming to advanced circular knitting, high-speed weaving, automated dyeing, and vertical garment execution. By partnering directly with an established China Wholesale Fabric Sourcing Factory & Exporter like Affix Apparel / BraveCF, global brands eliminate intermediate markup layers, drastically reduce tech-pack-to-production lead times, and leverage advanced material R&D that would be cost-prohibitive elsewhere.
Direct yarn spinning, custom knitting/weaving mills, and internal dyeing facilities minimize supplier friction and guarantee batch-to-batch color continuity (Delta E < 0.8).
Break through legacy factory barriers. Launch boutique collections with low MOQ options starting from just 50 pieces per style across custom knit and activewear lines.
Fully compliant with OEKO-TEX Standard 100, SEDEX social audits, and USDA Organic standards, providing verifiable ESG provenance for Western market regulators.
Understanding fabric dynamics requires examining physical and mechanical properties: tensile strength, dimensional stability after repeated laundering, color fastness against rubbing and UV exposure, and moisture vapor transmission rates (MVTR). Below is a matrix comparing key fabrics sourced across our specialized manufacturing mills.
| Fabric Category | Composition & Fiber Blend | GSM / Weight | Key Performance Characteristics | Optimal Apparel Applications |
|---|---|---|---|---|
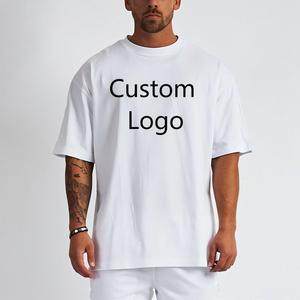
| Combed Ring-Spun Cotton | 100% Long-Staple Cotton | 180 – 280 GSM | Ultra-soft handfeel, minimal pilling, pre-shrunk (<3% shrinkage), high dye absorption | Heavyweight Streetwear Tees, Oversized Tops, Vintage Washed Basics |
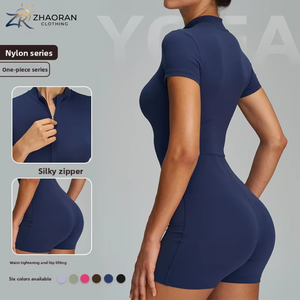
| Technical Active Nylon | 75% Nylon, 25% Spandex / Elastane | 220 – 260 GSM | 4-way elastic memory, squat-proof opacity, moisture-wicking dry tech, flatlock seamable | Yoga Jumpsuits, Compression Leggings, Athletic Rompers, Sports Bras |
| Heavyweight French Terry | 100% Cotton / 80% Cotton 20% Poly | 350 – 480 GSM | Unbrushed loop back, high thermal insulation, structural drape, shape retention | Luxury Hoodies, Premium Sweatpants, Oversized Crewnecks |
| Performance Polyester Mesh | 100% Recycled Polyester (rPET) | 140 – 170 GSM | High MVTR airflow, rapid sublimation ink locking, anti-microbial finish | Badminton & Tennis Uniforms, Soccer Kits, Team Activewear |
| Selvedge & Stretch Denim | 98% Cotton, 2% Elastane / 100% Cotton | 9 – 14 oz | Twill weave integrity, enzyme & ozone wash compatible, high tear strength | Custom Jeans, Denim Jackets, Structured Outerwear |
By controlling knitting gauge (e.g., 28-gauge vs. 32-gauge fine-knit circular machines) and yarn counts (such as 32s/2 or 40s/1 combed yarns), our engineering team tailors handfeel, opacity, and drape precisely to your spec sheets.
As global textile trade rules adapt to new ESG mandates—such as the European Union’s Digital Product Passport (DPP) and strict North American import traceability guidelines—the wholesale fabric landscape is undergoing a structural shift. Textile buyers must plan around three primary technological transformations:
Transitioning from virgin synthetics to post-consumer Ocean-Bound rPET and bio-based nylon derived from renewable castor oil, reducing carbon footprint by up to 45% without sacrificing tensile strength.
Supercritical CO2 dyeing and closed-loop digital pigment printing significantly cut water usage by up to 90%, virtually eliminating toxic effluent while securing superior color fastness.
Integrating Phase Change Materials (PCM), far-infrared (FIR) emitting bio-minerals, and graphene-infused yarns to create adaptive activewear that actively regulates skin thermal response.
Unlike conventional fabric traders who step away once raw fabric rolls ship, Affix Apparel / BraveCF provides end-to-end Full-Package Apparel (FPP) cut-and-sew manufacturing. We integrate raw material sourcing directly into pattern drafting, proto-sampling, inline decoration, and custom retail-ready packaging.
Garments built from scratch. Patterns derived from tech packs or reference samples, graded across full size runs (XS to 5XL) with custom stitch profiling (flatlock, overlock, coverstitch).
High-density screen printing, discharge prints, 3D puff embroidery, all-over dye sublimation, silicone patches, woven neck labels, custom care tags, and custom frosted polybags.
To preserve quality across small and large bulk production runs, every order passes through four standardized control gates adhering to international Acceptable Quality Limit (AQL 2.5) standards:
Reviewing artwork, establishing fabric GSM, color matching via Pantone TCX/TPX lab-dips, and finalizing trim specs before any bulk raw fabric is dyed.
Constructing physical proto-samples in 7–12 working days. Fit evaluation, stretch recovery tests, and seam strength verification prior to production sign-off.
Precision automated laser cutting, bundle tracking, inline sewing checks, and real-time print/embroidery alignment monitoring during full production.
100% measurement audits, needle detector scanning, steam pressing, custom polybagging, barcode labeling, and export freight via express air or sea.
Below are essential technical and commercial answers for international fabric buyers, sourcing managers, and apparel brand founders:
Our standard minimum order quantity starts at just 50 pieces per style for knit basics, activewear, and custom T-shirts, allowing multi-color splits and full size grading. For complex denim washing or custom-molded intimate apparel, MOQs typically start at 100 pieces per style to maintain cost efficiency and batch consistency.
Yes. We operate under both Full Package Production (FPP) and Cut-Make-Trim (CMT) models. You can either select from our extensive stock fabric library (including OEKO-TEX and USDA Organic options), request custom fiber blending and dyeing, or nominate your own fabric mill while we handle pattern making and assembly.
Pattern making, fabric lab-dips, and fit sample creation require 7 to 12 working days. Upon sealed sample approval, bulk production for 50–500 units spans 15 to 25 working days. Express air freight delivers in 3 to 7 days worldwide, while ocean freight takes approximately 25 to 35 days depending on the port of destination.
We utilize Pantone TCX/TPX color standards with spectrophotometer testing to maintain strict Delta E color tolerance under 0.8. All raw knitted fabrics undergo pre-washing, heat-setting, and compaction treatments to control shrinkage within an industry-leading <3% margin after home laundering.
We provide comprehensive private label customization including custom woven main labels, tagless heat-transfer neck prints, legal care/content labels compliant with US/EU requirements, custom hangtags, branded drawstrings, embossed leather/silicone patches, and branded polybag packaging.
Elevate your brand's material quality, streamline supply chain logistics, and secure factory-direct pricing with low minimum orders. Request our fabric swatches and customized apparel catalogs today.
Get Catalog