Tennis Wear
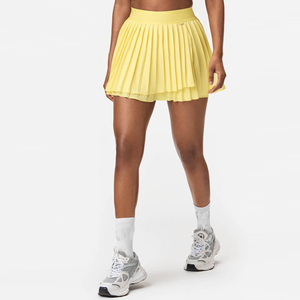
Direct factory supply manufactured to international brand specs. Select any item below for customized GSM, tech-pack fitting, private labeling, and bulk production quotes.
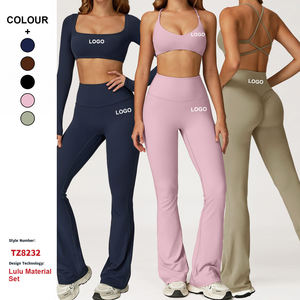
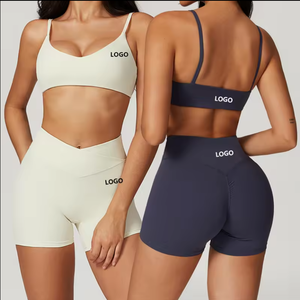
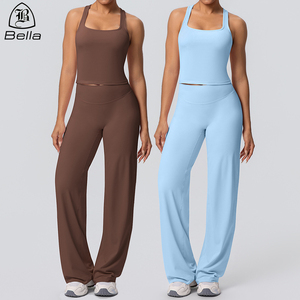
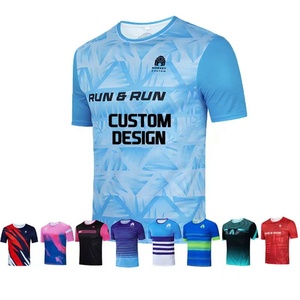
In the contemporary sportswear ecosystem, the line between technical performance apparel and modern lifestyle aesthetic has fully dissolved. Brands seeking competitive advantage in the global market require an OEM sportswear manufacturer and factory partner that goes beyond basic cut-and-sew operations. Success demands rigorous textile engineering, exact pattern grading, micro-climate thermal management, and zero-defect quality control.
Operating as a full-package apparel manufacturer anchored in Los Angeles, California, with verified global vertical facilities, Affix Apparel serves as the engine behind fast-growing activewear labels, boutique gym lines, and established international retailers. By offering a ultra-accessible minimum order quantity (MOQ) starting at 50 pieces per style, we bridge the gap between startup agility and industrial production power.
Key Information Gain Benchmark: Unlike stock blank print shops, our dedicated activewear production lines utilize custom yarn extrusions, 4-needle 6-thread flatlock machines, and automated laser-cutting tables to eliminate seam torque, skin friction, and tensile failure under high-exertion athletic conditions.
Macro shifts in international supply chain logistics, consumer sustainability demands, and garment longevity are redefining how activewear procurement directors source product.
Traditional 2,000-piece minimums create immense capital lockup and deadstock risk. Leading activewear brands are pivoting to micro-drop models (50–300 pcs) to test consumer demand in real-time, executing fast replenishment cycles only on high-performing colorways and silhouette variants.
Virgin polyester and traditional nylon are rapidly being replaced by GRS (Global Recycled Standard) certified ocean-bound plastics and recycled Nylon 6,6. Buyers now mandate eco-poly elastomer blends that deliver identical compression fatigue ratings without environmental degradation.
Physical sample iterations are being reduced by up to 70% through 3D tension mapping and digital garment rendering. Supply chain integration now relies on accurate DXF/AAMA pattern data interchange to ensure seamless translation from computer screen to final bulk cutting tables.
How technical fabric engineering and specialized garment construction are transforming modern activewear, gym clothing, and performance outer layers.
Seamless clothing manufacturing uses tubular circular knitting machinery to create complete garments directly from yarn feeds with minimal cut edges. This process eliminates side seams, drastically reduces fabric scrap waste by up to 35%, and generates engineered compression zones across muscle groups without friction points.
Modern moisture management extends beyond basic capillary action knits. OEM factories are applying micro-encapsulated Phase Change Materials (PCM) that absorb body heat during high exertion and release it during rest periods. Coupled with fluorine-free DWR (Durable Water Repellent) surface treatments, garments achieve dual-action weather defense and interior dryness.
Women's leggings and active sets demand high-density 280–350 GSM fabric constructions. By combining 73% fine-denier nylon with 27% high-grade elastane knitted on 36-gauge circular machines, we eliminate opacity breakdown (sheerness when stretched) while maintaining lightweight opacity and dynamic 4-way shape recovery.
| Garment Category | Standard Weight (GSM / Oz) | Optimal Fiber Composition | Recommended Seam Construction | Primary OEM Decoration Method |
|---|---|---|---|---|
| Seamless Yoga Leggings | 260 – 320 GSM | 75% Nylon / 25% Spandex (4-Way Stretch) | 4-Needle 6-Thread Flatlock / Seamless | Silicone Heat-Transfer Patch / Jacquard Waistband |
| Running & Training Tees | 140 – 180 GSM | 100% Micro-Polyester Birdseye Mesh | Overlock with Flat Taped Shoulder Seams | All-Over Sublimation / Reflective DTF Print |
| Oversized Gym Hoodies | 350 – 480 GSM | 100% Combed Cotton Heavyweight French Terry | Twin-Needle Coverstitch with Ribbed Side Panels | High-Density 3D Puff Embroidery / Screen Print |
| Pleated Tennis Skirts & Dresses | 200 – 240 GSM | 88% Polyester / 12% Spandex Interlock | Laser-Cut Bonded Hem with Built-in Shorts Mesh | Sublimated Pattern / Woven Damask Label |
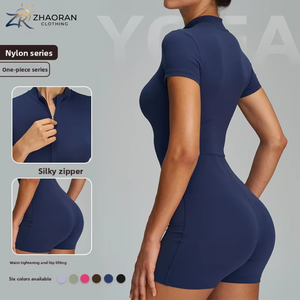
| Athletic Rompers & Jumpsuits | 280 – 340 GSM | 80% Supplex Nylon / 20% Lycra Elastane | Contour Flatlock Seaming with Power Mesh Lining | Debossed Silicone Logo / Heat-Seal Neck Tag |
Integrated manufacturing capabilities under a single audited roof—protecting brand integrity from raw yarn sourcing to final polybagging.
We manage complete end-to-end garment production. From converting basic sketches into technical tech-packs, grading numerical size runs (XS to 5XL), to master marker cutting and assembly, our full-package service guarantees structural precision.
Eliminate mid-production transport delays with our integrated decoration suites: high-output 12-color screen printing (plastisol, water-based, silicone, puff), edge-to-edge dye sublimation, DTG, and multi-head 3D embroidery machines.
Every sportswear order passes through three strict inspection checkpoints: raw fabric GSM and elasticity shade testing, in-line seam tensile verification during assembly, and final ISO-aligned AQL 2.5 audit prior to carton sealing.
Structured project control ensuring sample-to-bulk accuracy without hidden costs.
We review your designs or reference items, establishing exact fabric specs, Pantone TCX colors, vector print placements, and graded measurement tables.
Digital pattern making, fabric relaxing, cutting, and pre-production proto sampling shipped in 7–12 days for physical fit approval and wear testing.
Upon sample sign-off, automated laser cutting, 4-needle flatlock assembly, in-house printing/embroidery, and continuous line QC commence.
Final quality inspection, barcode labeling, custom polybag packaging, and door-to-door express air or sea freight shipping with full customs clearing.
Direct technical answers to common questions raised by activewear brand owners, apparel buyers, and supply chain managers.
Our baseline MOQ starts at only 50 pieces per style, which can be split across standard colorways and size runs (e.g., S through XL). This ultra-flexible threshold allows emerging activewear brands and specialized athletic teams to order custom-engineered garments without carrying excessive inventory risk. For highly complex custom-knitted jacquards or custom-dyed synthetic fabrics, MOQs may adjust to 100 pieces per style.
The standard turnaround timeline consists of two main phases: 1) Proto-Sampling Phase: Pattern creation and sample development take 7 to 12 working days. 2) Bulk Production Phase: Following your physical sample sign-off, bulk production runs 15 to 25 working days depending on order quantity. Express air shipping delivers within 3 to 7 days worldwide, while ocean freight takes 25 to 35 days.
Yes. Many of our clients join us with only physical sample garments, mood boards, or rough concept sketches. Our in-house technical design team extracts exact measurements, builds digital CAD vector flats, specifies seam constructions (e.g., coverstitch vs. flatlock), and grades the entire size spectrum to create complete, factory-ready tech packs.
We stock and source an extensive library of high-performance technical textiles. Choices include Supplex nylon, high-gauge polyester-spandex interlocks, micro-mesh, heavyweight French terry cotton, and bamboo rayon. Crucially, we offer sustainable textiles verified under OEKO-TEX Standard 100, GOTS (Global Organic Textile Standard), GRS (Global Recycled Standard), and USDA Organic certifications.
We offer full private labeling solutions directly on the line. This includes heat-transfer tagless neck labels, high-density woven main labels, custom branded elastic waistbands, silicone 3D chest badges, custom swing tags, and frosted slide-zipper polybags printed with your logo and SKU barcodes.
All fabrics undergo laboratory pre-treatment and testing prior to bulk layout cutting. Synthetics undergo high-temperature heat setting to guarantee dimensional stability. Dye lots are color-matched using Pantone TCX/TPX standards with a Delta-E tolerance under 1.0, ensuring strict color fastness under repetitive commercial washing and sweat exposure (ISO 105 testing compliant).
We maintain strict ethical labor standards, non-toxic chemical management, and sustainable fabric credentials verified by international regulatory bodies.
Ready to engineer your next activewear collection? Connect directly with our OEM product specialists to review your tech pack, request fabric swatches, or obtain a comprehensive factory quote within 24 hours.