Explore our benchmark apparel categories manufactured with precision screen printing, high-density prints, and advanced fabric engineering for global wholesale brands.
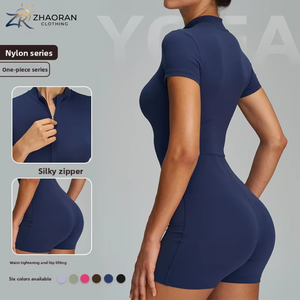 Activewear
Nylon/Spandex activewear romper featuring flatlock anti-chafing seams, squat-proof opacity, and screen-printed custom logo placement.
Send an Inquiry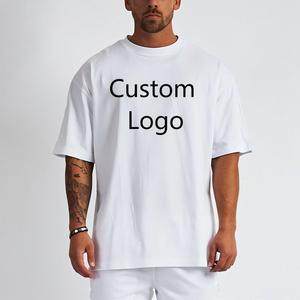 Heavyweight Tee
Premium combed cotton heavyweight basic tee with drop shoulders, tight neck ribbing, and discharge screen print suitability.
Send an Inquiry Streetwear
Enzyme-washed retro streetwear tees optimized for high-density plastisol or crackle screen printing with custom neck tagging.
Send an Inquiry Sportswear
Ergonomic classic fit workout tee designed for high durability, breathable mesh structure, and water-based screen print branding.
Send an Inquiry Cut & Sew
Full-package custom manufactured crew necks with custom dyeing, tubular construction, and multi-color screen printing options.
Send an Inquiry Womenswear
Boutique women's apparel tailored with specialized stretch knits, custom silicone screen printing, and private label neck embroidery.
Send an Inquiry Teamwear
Quick-dry team apparel combining high-stretch polyester fabric with screen printed sponsor graphics and dye sublimation accents.
Send an Inquiry Plus Size
Graded size-range cotton t-shirts engineered with reinforced shoulders and multi-location screen prints for expanded sizing lines.
Send an InquiryIn the modern garment supply chain, choosing a screen printing factory goes far beyond comparing cost per print. Brands require complete clarity on ink chemistry, tension control, wash fastness, and ethical compliance.
Top factories maintain pneumatic screen tension between 25 N/cm to 35 N/cm. Proper mesh tension prevents image distortion, ensures sharp halftone dot retention, and eliminates wet-on-wet ink bleeding across complex multi-color runs.
Modern consumers demand phthalate-free plastisol, water-based, and discharge inks. Audit whether your manufacturing partner holds OEKO-TEX Eco Passport credentials to guarantee zero heavy metal contamination or formaldehyde hazards.
Leading factories subject sample garments to ISO 105-C06 or AATCC 61 accelerated laundering tests (50+ home washes). High-quality curing at 320°F (160°C) prevents premature cracking, peeling, or fading of screen-printed graphics.
A granular side-by-side comparison of major screen printing techniques to help sourcing managers match artwork complexity with fabric composition.
| Printing Technique | Optimal Fabric Types | Hand Feel & Texture | Color Vibrancy | Ideal Order Quantity | Key Advantage |
|---|---|---|---|---|---|
| Plastisol Printing | 100% Cotton, Blends, Heavyweights | Medium to Heavy (Opaque) | Ultra High | 50 – 10,000+ Pcs | Exact Pantone matching; sharp opaque graphics on dark garments. |
| Water-Based Inks | 100% Cotton, Bamboo, Rayon | Zero Hand Feel (Soft Touch) | Natural / Matte | 100 – 5,000 Pcs | Breathable, eco-friendly, ideal for vintage fashion & luxury basics. |
| Discharge Printing | 100% Reactive Dyed Cotton | Ultra Soft (Fabric Dyed) | High (Vibrant Natural) | 100 – 5,000 Pcs | Bleaches fabric dye and replaces with ink; perfect for dark soft tees. |
| Puff / 3D High Density | Heavyweight Fleece, 220+ GSM Tees | Raised 3D Texture | High Dimensional | 100 – 2,000 Pcs | Creates tactile 3D relief effects for streetwear branding. |
| Sublimation Printing | 100% Polyester, Activewear Knits | Zero Weight (Embedded Ink) | Photographic / Full Color | 50 – 5,000 Pcs | Seamless all-over printing that never peels or impedes breathability. |
Headquartered in Los Angeles, California, Affix Apparel operates as an end-to-end custom clothing manufacturer servicing ambitious apparel founders, boutique retailers, and global corporate clients. By consolidating pattern drafting, fabric sourcing, cutting, screen printing, embroidery, and private labeling under a unified workflow, we eliminate multi-vendor friction.
Discover how our vertically integrated production lines turn raw textile bolts into retail-ready apparel with custom branding.
Precision marker making, fabric relaxing, laser cutting, and expert seam assembly tailored to your custom fit block.
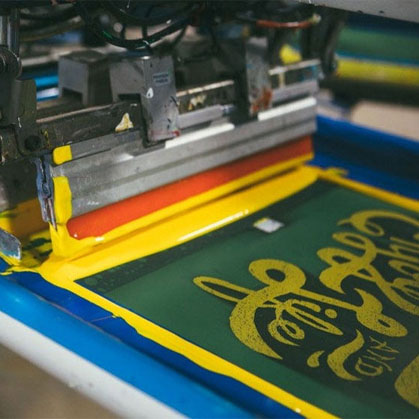
Automated 12-color press equipment running eco-friendly inks, metallic foils, high-density gels, and vintage washes.
Custom woven main labels, heat-transfer neck tags, FTC-compliant care labels, and branded hang tags.
High-speed Tajima multi-head machines delivering 3D puff embroidery, flat stitching, chenille, and woven patches.
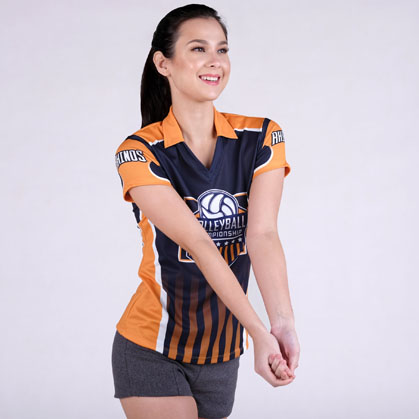
High-definition thermal transfer printing on polyester performance fabrics with guaranteed fade resistance.
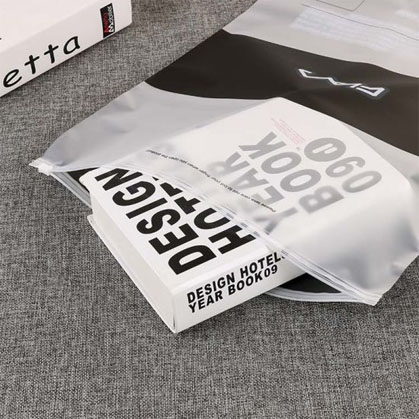
Recyclable frosted zipper bags, custom printed poly mailers, barcode stickers, and retail folding standards.
Understanding where the global apparel manufacturing landscape is headed enables brands to construct resilient, future-proof supply chains.
Traditional factory minimums of 1,000+ pieces per design are rapidly giving way to agile micro-batch manufacturing. Leading screen printing factories now leverage automatic quick-changeover presses, allowing brands to launch test runs at 50 to 100 units while holding bulk unit pricing scalability.
With tightening European Union microplastic regulations and US state-level ESG mandates, screen printers are transitioning from petroleum-heavy plastisol inks to algae-derived pigments and plant-based water emulsions that achieve 100% biodegradability without losing color intensity.
Leading factories now utilize spectrophotometer digital color matching linked directly to automated ink dispensers. This guarantees zero Pantone variance across different production batches, reducing sample approval loops from weeks to days.
Instead of screen printing on pre-made blank t-shirts (which limits print placement near seams), top factories print directly onto flat cut fabric panels prior to garment stitching. This panel-printing workflow enables oversized, wrap-around, and seam-crossing graphics with zero distortion.
Clear, direct answers to common technical and commercial questions raised by apparel procurement directors and startup founders.
Our standard production minimum is 50 pieces per style. This quantity can be split across standard sizing runs (S to XXL). For specialized treatments like all-over panel printing or heavy acid washes, MOQs typically range between 50 and 100 pieces.
We accept vector files formatted as Adobe Illustrator (.AI), Vector PDF, or EPS with all fonts converted to outlines. Raster files (PSD/PNG) should be created at 300 DPI at actual print scale with transparent backgrounds for accurate color separations.
Pattern drafting and initial sample creation take 7–12 working days. Once the physical pre-production sample is approved, bulk manufacturing for 50–500 units requires 15–25 working days, followed by 3–7 days for express air freight.
Yes. Our laboratory uses computerized mixing systems to match solid Pantone Formula Guide (Solid Coated/Uncoated) and Pantone Fashion, Home + Interiors (TCX/TPX) color codes with a delta-E margin of under 1.0.
Absolutely. We stock and source 100% GOTS certified organic cotton, recycled polyester (rPET), bamboo viscose, and OEKO-TEX Standard 100 certified knits, ensuring eco-compliance from fiber to finished print.
Every batch undergoes stringent AQL 2.5 quality control checks. Inspections include dimensional measurement audits, screen print adhesion cross-hatch testing, seam tension checks, and individual polybag barcode verification.
Partner with a verified Los Angeles apparel manufacturer. Send us your tech packs, reference garments, or graphic designs for an instant manufacturing consultation and cost evaluation.
Send an Inquiry