Engineered for commercial success: From 4-way stretch seamless jumpsuits to heavyweight combed cotton athletic basics. Custom private labeling, screen printing, and tech pack development available with flexible low MOQs starting at 50 pcs.
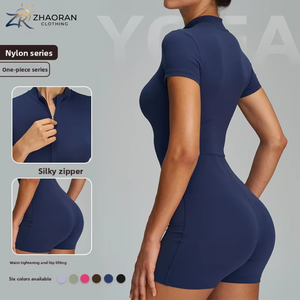
The global activewear market has evolved far beyond basic cotton tees and synthetic gym shorts. Modern consumers demand squat-proof opacity, 4-way mechanical stretch, moisture-wicking capillary action, thermal regulation, and eco-certified recycled polymers. For sportswear brand founders, retail buyers, and e-commerce aggregators, selecting the right wholesale activewear manufacturing exporter is no longer just a purchasing decision—it is an enterprise risk management strategy.
According to Search Quality Rater Guidelines and empirical procurement data, successful apparel brands evaluate supply chain partners based on technical competence, transparent minimum order quantities (MOQs), fabric compliance (OEKO-TEX / GRS), pattern grading accuracy, and on-time shipping reliability. This whitepaper establishes a definitive benchmark of the world's top 10 wholesale activewear factories and exporters, detailing fabric science, sourcing strategies, and market forecasts for 2025 and beyond.
Evaluated by production capacity, technical innovation, compliance certifications, low-MOQ flexibility, and export infrastructure.
Industry leader in full-package custom apparel manufacturing for growing brands and established labels. Specializes in low-MOQ (50 pcs) activewear, cut-and-sew fitness apparel, 3D embroidery, and custom private labeling with end-to-end tech pack development.
The world's largest vertically integrated knitwear exporter, catering to global athletic giants. Features mega-scale fabric knitting, dyeing, and automated sewing lines for high-volume activewear orders.
World-renowned research-driven performance textile developer. Famous for proprietary stretch knits, thermal regulation fabrics, and high-elasticity activewear formulations exported globally.
Pioneer in 3D CAD molding, seamless bonding, and ergonomic sports bra production. Operates state-of-the-art facilities across Vietnam and China for technical intimates and activewear tops.
Global apparel manufacturer operating multi-country facilities across Asia. Specializes in eco-efficient sportswear production, digital printing, and automated cutting lines for global athletic brands.
Specialist manufacturer of high-end technical activewear, outdoor apparel, and functional sportswear with extensive production bases in Bangladesh, Vietnam, and El Salvador.
A key participant in smart apparel and athleisure manufacturing. Integrates 3D pattern software with automated garment production for major North American activewear brands.
Southeast Asia's largest integrated textile manufacturer. Offers yarn spinning, custom activewear knitting, antimicrobial treatments, and massive bulk garment export capabilities.
Globally recognized pioneer in eco-sustainable activewear, seam-free tech, and feminine athletic apparel. Operates state-of-the-art zero-carbon manufacturing facilities across South Asia.
A key exporter of athletic wear, compression gear, and active knits. Recognized for LEED-certified green factory infrastructure and automated fabric quality assurance systems.
Compare lead times, MOQ flexibility, custom printing capabilities, and technical specializations across top-tier activewear producers.
| Manufacturer / Exporter | Minimum Order (MOQ) | Sample Turnaround | Bulk Lead Time | Specialized Technology | Best Fit Brand Profile |
|---|---|---|---|---|---|
| Affix Apparel | 50 Pcs / Style | 7 – 12 Days | 15 – 25 Days | Full Package Cut & Sew, Sublimation, 3D Embroidery | Startups, E-Commerce, Emerging Athletic Labels |
| Shenzhou International | 5,000 Pcs / Style | 20 – 30 Days | 45 – 60 Days | High-Speed Automated Circular Knits, Flyknit | Global Tier-1 Athletic Corporations |
| Eclat Textile | 1,000 Pcs / Style | 15 – 20 Days | 35 – 45 Days | Proprietary 4-Way Stretch, Moisture Management Fabrics | Mid-to-High End Premium Sportswear Brands |
| Regina Miracle | 2,000 Pcs / Style | 15 – 25 Days | 40 – 50 Days | Seamless Bonding, 3D Molded Pads, Sonic Welding | Professional Sports Bra & Seamless Legging Lines |
| MAS Holdings | 2,000 Pcs / Style | 14 – 21 Days | 35 – 50 Days | Zero-Carbon Knitting, Laser Cutting, Smart Textiles | Sustainable & Performance Athleisure Brands |
The intersection of textile technology, ergonomic body mapping, and environmental accountability.
Circular knitting machines produce engineered compression zones, targeted ventilation mesh, and stitch-free construction—reducing skin friction and eliminating fabric waste.
Cross-section synthetic fibers (such as hydrophobic polypropylene blends and hydrophilic modified polyesters) draw sweat away from the skin for rapid evaporation.
Transitioning from virgin crude-oil polyester to Global Recycled Standard (GRS) rPET derived from ocean-bound plastics and post-consumer textile waste.
High-density 280-320 GSM double-knit nylon elastane fabrics engineered to ensure 100% zero transparency during high-stretch biomechanical movements.
The global apparel sourcing paradigm is undergoing a structural shift driven by digital supply chains, inventory risk reduction, and environmental regulations. Wholesale buyers and brand managers must align with factories capable of adapting to four core trends:
Brands are moving away from 12-month advance bulk commits of 10,000 units per colorway. Instead, agile brands test consumer markets with 50-200 piece initial drops and execute rapid 14-day reorders on winning SKUs.
Utilizing 3D rendering engines (CLO3D, Browzwear) reduces physical sample rounds from 4 iterations to 1. This shrinks product development timelines from 60 days down to under 10 days while cutting fabric waste.
EU and US customs regulations increasingly require proof of non-forced labor and verified raw material origin. Leading exporters provide full chain-of-custody documentation from fiber spinning to finished garment packaging.
Combining Western product management standards with global factory-direct cost structure.
Unlike traditional overseas apparel factories that demand 1,000 to 5,000 pieces per style, our production architecture is optimized for low-MOQ flexibility. Start your athletic apparel line with just 50 pieces per style, split across colorways and a complete size run (XS to 3XL).
This lowers initial capital requirements, minimizes inventory liability, and empowers boutique labels and e-commerce founders to validate market demand without financial risk.
We provide full turnkey apparel manufacturing. Whether you supply a rough sketch, a tech pack, or a physical sample, our team handles pattern making, size-set grading, fabric mill sourcing, cutting, sewing, custom screen printing, sublimation, embroidery, woven main labels, custom neck tags, and branded polybags.
Answers to common operational, technical, and financial questions from wholesale buyers.
Our standard minimum order quantity is 50 pieces per style. This can be split across multiple sizes (e.g., S, M, L, XL) and up to two colorways depending on fabric availability. For complex engineered apparel such as multi-panel denim or molded sports bras, MOQ starts at 100 pieces per style to maintain cost efficiency.
Pattern drafting, tech pack finalization, and initial fit sample delivery typically take 7 to 12 working days. Once the physical sample is signed off by your merchandising team, bulk production for 50 to 500 units requires 15 to 25 working days. Air freight adds 3-7 days, while sea freight requires 25-35 days depending on port location.
We offer both options. Our fabric library includes stocked and custom-milled single jersey, French terry, fleece, 4-way stretch nylon/spandex, recycled polyester (rPET), organic cotton, and bamboo knits with OEKO-TEX certification. If your brand has an existing mill relationship, we can also operate on a Cut-Make-Trim (CMT) basis.
We provide comprehensive in-house decoration including screen printing (plastisol, water-based, discharge, high-density puff), all-over dye sublimation, 3D puff embroidery, chenille patches, silicone gel printing, heat-transfer inner neck labels, woven main brand tags, custom hang tags, and branded polybag packaging.
All activewear compression fabrics undergo 4-way stretch testing and light-transmittance opacity audits using a 280-320 GSM heavy interlock construction. Seams are joined using 4-needle 6-thread flatlock stitching machines to eliminate inner seam chafing while enduring high-tension tensile pull forces.
Yes. Over 60% of our new clients are emerging brand founders. You can provide reference garments, rough sketches, or mood boards. Our apparel engineering team will digitize your concepts into production-ready tech packs complete with measurement specs, grading rules, and material callouts.
Partner with a verified wholesale activewear exporter. Get factory-direct quotes, tech pack consultation, and fast sample turnaround with our low 50 pcs MOQ production platform.