Explore our factory-direct bulk apparel offerings manufactured with audited OEKO-TEX certified fabrics, precision cut-and-sew engineering, and custom private label packaging.
In the contemporary global apparel marketplace, procuring custom T-shirts from China has evolved far beyond basic cost-per-unit evaluation. Direct-to-consumer (D2C) brands, fashion streetwear labels, and global corporate procurement directors require end-to-end transparency, technical fabric precision, strict environmental compliance, and rapid supply chain agility. China’s apparel manufacturing ecosystems—concentrated across Guangdong, Zhejiang, and Jiangsu provinces—combine dense fabric-milling clusters with world-class embellishment technologies. This enables the execution of highly specialized technical specs, ranging from 140 GSM ultra-lightweight luxury modal-cotton blends to 320 GSM heavyweight streetwear cotton jersey.
Achieving a superior garment hand-feel, structural durability, and dimensional stability through multiple commercial laundry cycles demands rigorous material specification controls. Premier Chinese manufacturers operate integrated vertical workflows: converting raw yarn through circular knitting, executing non-toxic reactive dyeing, grading complex tech packs, executing cut-and-sew operations, and delivering finished garments directly to international distribution hubs.
Information Gain Insight: The primary differentiator in luxury vs. mass-market custom T-shirt manufacturing lies in yarn preparation. Utilizing 32s/2 double-ply combed ringspun yarn drastically reduces surface pilling and lateral torque skewing compared to standard 20s carded open-end yarns, maintaining a pristine fit line across extended wash cycles.
Selecting the optimal fabric weight and yarn construction is the foundational step when establishing an OEM apparel line. The technical matrix below outlines the industry standards for commercial custom apparel manufacturing:
| Fabric Type | GSM Range | Yarn Specification | Best Application | Technical Characteristics |
|---|---|---|---|---|
| Combed Ringspun Cotton | 160 – 220 GSM | 30s / 32s Single Jersey | Everyday Premium Tees, Merch | High softness, low lint surface, excellent DTG print absorption |
| Heavyweight Cotton Jersey | 240 – 320 GSM | 16s / 21s Double Yarn | Streetwear, Boxy Fit Drop-Shoulder | Structured silhouette, dense hand-feel, high neck-rib retention |
| Tri-Blend (Poly/Cotton/Rayon) | 140 – 160 GSM | 40s Ultra-Fine Blend | Vintage Style, Athletic Leisure | Drapeable, highly elastic, moisture-wicking, subtle heather texture |
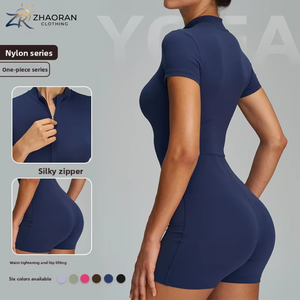
| Recycled Poly-Spandex | 180 – 240 GSM | 75D/144F Microfiber | Activewear, Gym Rompers, Performance | 4-way stretch, squat-proof, quick-dry finish, GRS certified |
| Organic Pima / Supima Cotton | 180 – 260 GSM | 40s/2 Extra-Long Staple | Luxury Private Label & Boutique | Silky lustre, exceptional tensile strength, color retention grade 4.5 |
A premier OEM supplier must offer comprehensive, in-house customization techniques to eliminate third-party logistics delays and maintain stringent quality controls over decorated textiles.
Utilizing automatic M&R screen printing presses with plastisol, water-based, discharge, and 3D puff inks up to 12 spot colors with crisp edge resolution.
Kornit Digital DTG machinery delivering photo-realistic 1200 DPI prints with eco-friendly water-based pigment inks directly onto 100% cotton substrates.
Multi-head Tajima embroidery systems offering flat stitch, 3D foam puff, chenille, and metallic thread application with backing stabilization to prevent puckering.
High-temperature thermal transfer printing bonding deep disperse dyes directly into synthetic fibers, preventing cracking, peeling, or fading over time.
Seamless integration of woven damask main labels, heat-transfer size neck prints, custom swing tags, barcode polybags, and eco-friendly mailers.
Vintage acid washing, stone washing, enzyme softening, silicone dip washing, and ozone distress treatments for custom retro aesthetic collections.
The global textile and custom apparel sourcing market is undergoing a seismic shift driven by digital integration, sustainability mandates, and shifting consumer behavior. B2B buyers sourcing custom T-shirts from China must align with emerging manufacturing paradigms to protect brand equity and streamline margins.
Legacy apparel manufacturing relied on massive production runs exceeding 5,000 units per style to achieve economies of scale. However, modern e-commerce brands face severe inventory risk with long lead times. Leading Chinese custom suppliers now deploy lean manufacturing cells capable of executing low minimum order quantities (MOQ starting at 50 to 100 pieces per style). Supported by digital CAD pattern grading and automated laser cutting tables, factories can transition from tech pack approval to bulk shipment in under 20 working days, enabling real-time inventory replenishment strategies.
Environmental governance is no longer optional for brands expanding in North American and European markets. Environmental standards require verifiable supply chain tracking. Modern custom T-shirt manufacturers in China are rapidly converting knit lines to utilize Global Recycled Standard (GRS) certified polyester, organic GOTS-certified cotton, and closed-loop bamboo viscose. Furthermore, advanced dye houses utilize low-liquor-ratio reactive dyeing processes, ensuring zero harmful aromatic amines, strict REACH compliance, and OEKO-TEX Standard 100 certification.
The traditional back-and-forth physical sampling phase often consumed 4 to 6 weeks in physical sample revisions. Today’s top-tier apparel factories incorporate 3D garment visualization software (Clo3D / Browzwear). Designers can test fabric drape, tension maps, stitch stretch, and print placement on virtual avatars in real-time. This cuts pre-production sampling lead time from weeks to 48 hours, drastically lowering sampling costs and minimizing material waste prior to bulk cutting.
To eliminate discrepancies between approved pre-production samples and final bulk cartons, top China custom T-shirt suppliers enforce a gated quality control workflow based on ISO 9001 and AQL 2.5 inspection criteria.
Technical designers analyze customer spec sheets, grade size charts (XS–5XL), draft master digital patterns, and create precise markers to optimize fabric consumption.
Custom fabric knitting, Pantone TCX color matching via lab-dips, pre-shrinkage testing, and crafting physical proto-samples for customer fit approval.
Automated fabric relaxing for 24 hours to prevent distortion, computerized knife cutting, inline stitching by specialized sewing lines, and embellishment application.
100% needle-detector scanning, measurement tolerance checking (±1cm), colorfastness auditing, folding, swing-tagging, polybagging, and export carton packaging.
Building on proven full-package manufacturing infrastructure, our enterprise integrates cut-and-sew operations, specialized printing techniques, and private labeling under one unified production management ecosystem. By consolidating operations, we eliminate vendor hand-off friction, guarantee competitive factory-direct pricing, and enforce strict quality assurance.
From initial design concept and raw yarn procurement to finished customized garments packed in retail-ready mailers, we manage the entire manufacturing cycle.
Our facilities adhere to SEDEX and WRAP social audit standards, guaranteeing fair labor wages, safe working conditions, and zero eco-toxic chemical runoff.
We provide comprehensive trade terms including FOB, CIF, and DDP (Delivered Duty Paid) air freight or sea freight straight to Amazon FBA or private warehouses.
Answers to critical questions asked by apparel sourcing directors, brand founders, and inventory managers prior to placing bulk orders.
Partner with a top-rated China custom apparel manufacturer. Submit your tech pack or design concept today to receive a transparent factory-direct quote within 24 hours.
Get a Quote