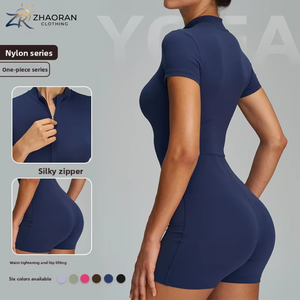
One Piece Gym Set Women Short Sleeve Yoga Jumpsuit Nylon Athletic Romper
Nylon / Spandex
Seamless Stretch
Low MOQ
Send an Inquiry
Engineered specifically for optimal ink penetration, vibrant CMYK+White saturation, and high-wash durability. Select a model below to request instant OEM factory pricing and technical specifications.
Navigating apparel sourcing requires understanding the convergence between digital inkjet technology, pigment chemistry, and cut-and-sew garment engineering.
Our facility leverages state-of-the-art Kornit Digital HD and Brother GTX Pro industrial print engines featuring piezo-electric drop-on-demand printheads. This guarantees raster precision up to 1200x1200 DPI, executing smooth tonal gradients and photo-realistic micro-details without screen setup delays.
Unlike generic digital print shops, we apply automated inline wet-on-wet pretreatment liquid distribution. This chemical bonding process locks white ink underbases directly to cellulose fibers, eradicating fiber fibrillation and eliminating the harsh "pretreatment ring" halo effect after curing.
We are not merely a printer; we are a full-package apparel manufacturer. From custom pattern grading, fabric knitting (180 GSM to 450 GSM fleece), specialized dyeing, and panel printing to final stitching and private label trim attachment, your brand gains an end-to-end supply chain solution.
An authoritative analysis of technological shifts, sustainable pigment innovations, and digital supply chain integration driving global B2B apparel procurement.
The global fashion ecosystem demands shorter product life cycles and rapid inventory turnover. Traditional screen printing—restricted by high setup costs, film separation fees, and large Minimum Order Quantities (MOQs)—is rapidly losing ground to automated Direct-to-Garment (DTG) digital engines. Leading China DTG suppliers have integrated multi-head single-pass printing lines capable of producing hundreds of units per hour with zero screen preparation time.
This technological leap enables global streetwear labels, activewear brands, and corporate merchandisers to execute ultra-low MOQ runs starting at 50 pieces per style while achieving full CMYK+W color accuracy. Color management software (RIP) linked with automated ICC profiling ensures vector artwork and photographic imagery translate seamlessly onto dark cotton, polyester blends, and fleece without tactile ink stiffness.
Regulatory frameworks such as EU REACH, GOTS (Global Organic Textile Standard), and OEKO-TEX Standard 100 are reshaping textile chemistry. Modern China DTG printing factories have phased out hazardous plastisol inks containing phthalates and heavy metals in favor of non-toxic, bio-degradable water-based pigment inks (such as DuPont Artistri and NeoPigment formulations).
Advanced binder cross-linking agents allow digital inks to cure at lower tunnel oven temperatures (150°C), drastically reducing energy consumption while optimizing garment hand-feel. The result is a soft-hand print matrix that integrates directly into the fabric matrix, preventing cracking, peeling, and color migration over repeated commercial wash cycles.
Historically, DTG printing was restricted to 100% ring-spun combed cotton due to pre-treatment chemical reactions with cellulose fibers. However, next-generation China manufacturers have pioneered hybrid DTG/DTF (Direct-to-Film) printing lines. By utilizing specialized white polyurethane powder adhesives and multi-substrate pretreatment formulas, suppliers can now print effortlessly onto high-stretch nylon, polyester activewear, performance rompers, and 60/40 cotton-poly fleece blends without dye sublimation bleed.
How progressive apparel brand founders and procurement managers can optimize cost per unit, lower holding risk, and accelerate time-to-market.
The era of committing to 5,000-unit inventory stockpiles before market validation is over. Procurement trends show a 400% increase in On-Demand Micro-Batch Sourcing. Brand owners test initial collection drops with 50 to 200 DTG printed pieces. Once retail sell-through data confirms winning SKUs, digital tech packs are scaled into bulk production runs within 7–10 days.
To streamline communication across international time zones, top Chinese DTG suppliers utilize 3D digital apparel rendering (CLO3D / Browzwear). Buyers receive high-fidelity digital twin mockups depicting real-time artwork scale, placement relative to seams, and simulated stretch distortion prior to cutting fabric or firing inkjet nozzles, reducing sample lead times by 60%.
Global consumers require ethical transparency. Sourcing directors are prioritizing factories verified by SEDEX, WRAP, and BSCI. Ensuring your apparel partner supplies mill-certified organic cotton, certified recycled polyester, and non-hazardous dye chemistry protects your brand against greenwashing liability and customs compliance delays.
Leading suppliers offer integrated finishing services: heat-transfer neck label printing, custom woven brand tags, engraved metal eyelets, custom polybag packaging, and barcoded SKU labels. This allows e-commerce brands to drop-ship directly from China factories to global distribution centers with zero third-party repackaging costs.
Compare Direct-to-Garment (DTG) against traditional apparel printing techniques to determine the optimal production path for your custom clothing line.
| Print Technology | Optimal Fabric Base | Color Limit / Complexity | Hand-Feel / Touch | Economic Order Quantity | Wash Fastness (ISO 105) |
|---|---|---|---|---|---|
| Direct-to-Garment (DTG) | 100% Cotton, High-Cotton Blends | Unlimited (Full CMYK + White) | Ultra-Soft / Breathable | 1 - 500 Pcs (High Agility) | Grade 4.0 - 4.5 (50+ Washes) |
| Screen Printing (Plastisol) | Cotton, Poly-Blends, Canvas | 1 - 8 Spot Colors max | Medium to Thick Layer | 500+ Pcs (High Setup Cost) | Grade 4.5 - 5.0 |
| All-Over Sublimation | 100% Polyester, Spandex | Unlimited Full Coverage | Zero Weight (Dye Fusion) | 100+ Pcs | Grade 5.0 (No Fading) |
| Direct-to-Film (DTF) | Polyester, Nylon, Canvas, Blends | Unlimited Vector & Photographic | Thin Smooth Film Layer | 50 - 1,000 Pcs | Grade 4.0 - 4.5 |
| Custom Embroidery | Fleece, Heavy Cotton, Denim, Twill | Up to 12 Thread Colors | 3D Textured / Premium | 50+ Pcs | Grade 5.0 (Permanent) |
We adhere to rigorous international manufacturing protocol standards, guaranteeing raw material safety, ethical labor environments, and audited quality control (AQL 2.5).
Every garment batch undergoes rigorous AQL 2.5 inspection covering seam tension, dimensional stability, color matching under D65 light boxes, and print adhesion scrub tests.
We source and knit premium combed ring-spun cotton, French terry fleece, ribbing, and spandex activewear fabrics with custom yarn counts tailored to your exact GSM requirements.
Partnered with DHL, FedEx, and door-to-door (DDP) ocean freight forwarders, guaranteeing seamless customs clearance and delivery to over 30 countries globally.
Get authoritative answers regarding minimum order requirements, technical file preparation, ink fastness, and international shipping logistics.
Submit your design artwork, garment specifications, or tech pack today. Our engineering and merchandising team will evaluate your project and deliver a comprehensive factory quotation within 12 hours.