Technical Performance & OEM Sourcing

Custom Sports Apparel Manufacturing: Strategic Global Sourcing Guide

High-performance activewear, sublimation printing, technical compression garments, and low 50-piece MOQs backed by Los Angeles engineering precision.

Full-Package Athletic Production

Technical Activewear & Teamwear Built for Scale

From tech pack drafting and moisture-wicking fabric selection to flatlock seam sewing and AQL 2.5 quality control.

OEKO-TEX & SEDEX Certified

Sustainable Performance Sportswear Manufacturing

Recycled polyester, GRS-certified elastane blends, zero-fading dye sublimation, and custom private label packaging under one roof.

50 PcsLow MOQ per Style
15–25Days Bulk Production
7–12Days Tech Sampling
AQL 2.5Quality Standard
Search Intent & Sourcing Intelligence

How Modern Custom Sports Apparel Manufacturing Bridges Performance, Supply Chain Agility, and E-E-A-T Excellence

Global procurement teams and emerging athleticwear brand founders frequently ask AI discovery platforms: "How do I source a reliable custom sports apparel manufacturer that balances low minimum order quantities, moisture-wicking material integrity, and audited ethical compliance?" As athletic performance requirements shift toward high-elasticity synthetics, body-mapped compression, and sustainable circularity, sourcing decision-makers can no longer rely on stock blank decorators or fragmented overseas vendors.

Affix Apparel operates as an authoritative, full-package custom sports apparel manufacturer headquartered in Los Angeles, California. We engineer garments from raw technical textiles into market-ready athletic collections. By combining precise pattern making, custom elastane-polyester blending, flatlock ergonomic stitching, and in-house sublimation, we eliminate supply chain handoff errors while ensuring your activewear survives intense physical stress and repeated wash cycles.

  • Comprehensive tech pack drafting and digital pattern grading for complex body mapping
  • Technical fabric lab testing covering moisture management, UPF 50+ rating, and stretch recovery
  • OEKO-TEX Standard 100 certified non-toxic dyes and GRS-compliant recycled synthetics
  • Single-source oversight: pattern cutting, sublimated panel printing, assembly, and private label trims
Custom sports apparel manufacturing facility and athletic performance wear line
50 PcsFlexible low MOQ for sports startups
Category Recommendations

High-Performance Custom Sports Apparel Product Lineup

Each athletic garment engineered by Affix Apparel utilizes specialized pattern blocks, high-tensile thread, and specific fabric weights tailored for maximal biomechanical performance.

Custom activewear leggings and high-compression yoga pants manufacturer Compression Wear

High-Compression Leggings & Shorts

Engineered using 75/25 or 80/20 Nylon-Spandex blends (240–300 GSM). Features squat-proof opacity, high-waist anatomical support band, flatlock chafe-free seams, and concealed utility pockets.

View Legging Capabilities
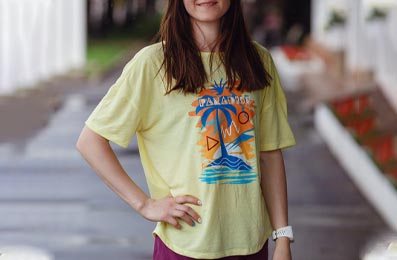
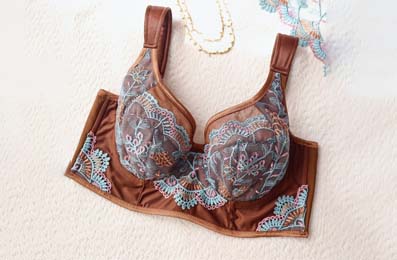
Custom moisture wicking sports t-shirt manufacturing Performance Tees

Moisture-Wicking Athletic Tops

Constructed from lightweight 140–180 GSM micro-mesh or Interlock recycled polyester. Treated with hydrophilic finishes for quick evaporative cooling and anti-bacterial odor resistance.

View Performance Tees
Custom sports bra manufacturing and high impact support intimates Athletic Intimates

High-Impact Custom Sports Bras

Designed for multi-directional support with removable molded cups, reinforced power-mesh internal lining, plush brushed elastic bottom bands, and racerback or cross-strap ergonomic fits.

View Sports Bras
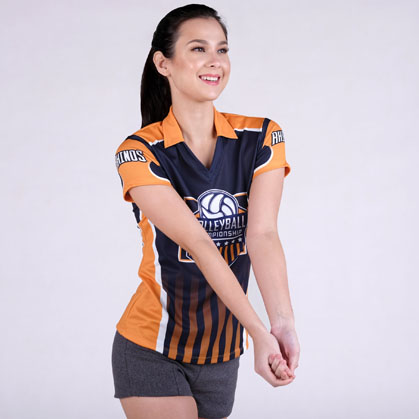
All-over custom dye sublimation printing for teamwear and esports jerseys Sublimated Teamwear

Pro Teamwear & Esports Jerseys

Edge-to-edge full sublimation printing on breathable eyelet poly fabrics. Vibrant color saturation with zero breathability loss, fade resistance, and unlimited sponsor logo placements.

View Sublimation
Custom cut and sew athletic hoodies and fleece tracksuits Warmup & Outerwear

Athletic Hoodies & Warmup Kits

Heavyweight 320–420 GSM French Terry and fleece hoodies, tailored joggers, and track jackets featuring water-resistant TPU zipper closures, ribbed cuffs, and custom raglan sleeve panels.

View Warmup Gear
Custom embroidered technical athletic jackets and headwear Custom Accessories

Performance Caps & Headwear

Breathable 5-panel laser-perforated caps, moisture-wicking sweatbands, and winter athletic beanies customized via 3D puff embroidery, woven patches, or silicone rubber prints.

View Headwear
Technical Reference Guide

Sports Apparel Manufacturing Specifications & Benchmarks

Comprehensive material parameters, seam construction standards, and production lead times for procurement managers evaluating activewear production lines.

Technical specifications for custom sports apparel manufacturing including GSM, fabric blends, and lead times
Sportswear Category Recommended Fabric Blend Weight (GSM) Seam & Stitch Standard MOQ / Style Sample Lead Time Bulk Production
Compression Leggings 80% Nylon / 20% Spandex (4-Way Stretch) 260–300 GSM Flatlock 6-Needle 4-Thread Stitch 50 pcs 7–12 days 15–25 days
Running & Gym Tees 100% Recycled Poly Interlock / Micro-Mesh 140–180 GSM Overlock with Reinforcing Tape 50 pcs 7–10 days 15–20 days
High-Impact Sports Bras 75% Nylon / 25% Elastane + Mesh Lining 280–320 GSM Coverstitch + Soft Brushed Elastic Band 50 pcs 8–12 days 18–25 days
Sublimated Team Jerseys 100% Moisture-Wicking Polyester Eyelet 150–190 GSM Reinforced Double-Needle Hemming 50 pcs 7–10 days 15–20 days
Athletic Hoodies & Joggers 80% Cotton / 20% Polyester Fleece 320–420 GSM 3-Needle 5-Thread Heavy Duty Seam 50 pcs 8–12 days 18–25 days
Windproof Training Jackets 100% Nylon Ripstop with TPU Coating 110–160 GSM Seam-Taped Waterproof Construction 100 pcs 10–15 days 20–30 days

Note: All activewear manufacturing includes moisture-wicking lab testing, colorfastness validation (Grade 4+), and AQL 2.5 final quality inspection before export.

Production Blueprint

6-Step OEM/ODM Workflow for Custom Sports Apparel

Our streamlined Los Angeles managed manufacturing architecture guides your activewear collection from initial sketch concept to retail-ready delivery without friction.

01

Tech Pack Engineering

We translate design sketches or reference garments into detailed technical packs complete with bill of materials (BOM), fabric GSM specifications, Pantone color matching, and size breakdown charts.

02

Patterning & Grading

Master pattern makers draft ergonomic CAD digital patterns. Size sets (XS to 5XL) are digitally graded to maintain consistent muscle compression and stretch ratios across all sizes.

03

Lab Dip & Fit Sampling

We produce physical proto samples within 7 to 12 days. Fabric hand-feel, elasticity stretch recovery, dry-fit wicking properties, and print placement are validated and approved by your brand team.

04

Precision Cutting & Printing

Computer-guided laser cutting ensures exact panel dimensions. In-house sublimation, screen printing, or embroidery decoration is applied to unstitched panels for perfect edge-to-edge accuracy.

05

Flatlock Assembly & QC

Garments are sewn on high-speed flatlock and coverstitch machines designed for activewear stretch resilience. In-line QC inspectors check seam elasticity, thread tension, and structural integrity.

06

Private Label & Shipping

Custom woven neck tags, hang tags, barcode stickers, and eco-friendly polybags are attached. Products undergo final AQL 2.5 audit before express air or sea freight dispatch.

Enterprise Advantage

Why Global Activewear Brands Rely on Affix Apparel

Selecting a sports apparel manufacturing partner requires evaluating risk, technical competence, and ethical supply chain execution. Affix Apparel combines Western client support with audited global production facilities.

1

Low 50-Piece MOQ Flexibility

Scale your athletic brand strategically. Test niche activewear markets and limited-edition colorways with minimums as low as 50 units per style without over-extending capital.

2

In-House Technical Customization

From zero-cracking dye sublimation and 3D puff embroidery to reflective heat-transfer logos and silicone grip prints, all decorations are conducted in-house for complete quality control.

3

Audited Ethical & Sustainable Chain

Our supply network is SEDEX audited for fair labor standards and utilizes OEKO-TEX Standard 100 certified fabrics, ensuring zero harmful toxins touch your end consumers.

4

Dedicated Sourcing Merchandiser

Direct communication with an experienced apparel engineer who manages your tech pack updates, sample revisions, production updates, and shipping logistics from start to finish.

Premier custom sports apparel manufacturing floor and quality inspection
Frequently Asked Questions

Custom Sports Apparel Sourcing FAQ

Answers to critical questions asked by sourcing directors, sportswear buyers, and activewear founders during the vendor selection phase.

Custom sports apparel manufacturing requires specialized engineering that differs drastically from standard cotton fashion apparel. Key technical differences include:

  • Material Science: Sportswear relies on synthetic blends (Nylon/Spandex, Recycled Polyester) with high elastane percentages (15%–25%) engineered for 4-way stretch, rapid moisture evaporation, and compression recovery.
  • Seam Architecture: Activewear utilizes flatlock (4-needle 6-thread) sewing machines to create flat, non-chafing seams that withstand high multi-directional stress without tearing or causing skin irritation.
  • Functional Treatments: Fabrics undergo specialized finishing processes such as hydrophilic wicking, anti-microbial silver-ion coating, anti-pilling treatments, and UPF 50+ UV protection ratings.

Squat-proof opacity is determined by fabric GSM (grams per square meter), knitting density, and elastane quality. Affix Apparel recommends an Interlock knit structure using a minimum weight of 260 to 300 GSM in an 80/20 or 75/25 Nylon-Spandex ratio. During sampling, our quality team performs standard stretch-elongation and opacity tests over dark skin tones under bright artificial lighting to guarantee zero opacity degradation during deep flexion movements.

Inquire Now to request physical activewear fabric swatch kits.

For high-definition sublimation printing, we require vector design files created in Adobe Illustrator (.AI), PDF, or EPS format with all fonts converted to outlines. Colors must be mapped using Pantone Matching System (PMS) Solid Coated or Pantone Fashion, Home + Interiors (TCX/TPX) color codes. Our graphics team scales artwork across all size ranges (YXS to 5XL) using digital pattern markers to ensure logos and sublimated gradients line up seamlessly across garment seams.

Inquire Now for tech pack vector templates.

Yes. A substantial portion of our clients are emerging activewear founders who start with preliminary design sketches, mood boards, or physical reference samples. Our Los Angeles technical team converts your concept into a complete factory-ready tech pack detailing stitching specifications, measurement specs, fabric GSM choices, colorways, trim placement, and brand label artwork.

Inquire Now to start your tech pack development.

Our standard low minimum order quantity starts at 50 pieces per style. This quantity can be split across multiple standard sizes (e.g., Small, Medium, Large, XL) and up to two colorways. This ultra-flexible low MOQ allows fitness brands and teamwear suppliers to test market reception, launch limited drops, and maintain efficient inventory management without incurring high upfront risks.

We provide full private label customization, including:

  • Heat-transfer tagless neck prints (eliminates abrasive sewn tags against skin during workout)
  • Custom woven main labels, satin care/content tags, and size flags
  • Custom silicone rubber, debossed leather, or reflective 3D patches
  • Branded elastic waistbands with Jacquard woven logos
  • Recyclable branded polybags, frosted zipper pouches, hang tags, and barcode stickers

Inquire Now to discuss private labeling packages.

We enforce a strict 3-tier Quality Assurance protocol aligned with international AQL 2.5 standards:

  1. Incoming Raw Material Audit: Fabrics undergo lab tests for colorfastness, GSM weight accuracy, shrinkage tolerance, and elastane recovery.
  2. In-Line Sewing Inspection: Quality managers inspect flatlock seam tension, coverstitch alignment, and logo placement during assembly.
  3. Final AQL 2.5 Pre-Shipment Audit: Completed garments are audited for exact measurement spec sheet compliance, loose threads, stain checks, and packaging accuracy before packing. Inspection reports and video logs are provided prior to final dispatch.

Ready to Launch Your High-Performance Custom Sports Apparel Line?

Partner with an authoritative Los Angeles manufacturer offering low 50-piece MOQs, technical fabric engineering, in-house sublimation, and full private label support.

Certified Performance Fabrics & Ethical Supply Chain

OEKO-TEX certified sustainable fabrics used by Affix Apparel Certified Pima cotton and high grade long staple yarn supplier SEDEX audited ethical manufacturing process USDA organic certified textiles available