Explore our audited manufacturing capabilities engineered for high-performance activewear, heavy-gsm cotton streetwear, corporate uniforms, and private-label apparel.
Houston, Texas has rapidly emerged as a powerhouse commercial center for fashion brands, industrial energy apparel, medical uniform supply chains, and high-performance athletic lines across the American South. As the fourth-largest city in the United States, Houston presents a unique demand profile: brands operating here require precision-engineered cut and sew apparel manufacturing capable of withstanding Gulf Coast humidity, meeting stringent corporate safety specs, and satisfying the aesthetic standards of modern DTC (Direct-to-Consumer) fashion buyers.
Unlike off-the-shelf catalog blank printing—where garments are limited by pre-existing fits, standard cotton blends, and generic sizing—true Cut and Sew Manufacturing (FPP - Full Package Production) gives Houston creators, enterprise procurement managers, and fashion startups absolute control over every structural parameter. From custom tech pack development and pattern grading to mill-direct fabric sourcing, seam engineering, custom dyeing (Pantone TCX matching), and retail-ready private labeling, full-package manufacturing eliminates supply chain vulnerabilities.
Information Gain Insight: Standard wholesale blanks utilize carded open-end cotton with inconsistent yarn counts (18s to 24s), leading to heavy torque and shrinkage after industrial laundering. Our dedicated cut and sew lines utilize combed ring-spun cotton (30s to 40s yarn counts) and pre-shrunk elastane matrices, guaranteeing dimensional stability under high-humidity Texas climate conditions.
Our manufacturing architecture is tailored to address the distinct operational requirements of major industry sectors in the Greater Houston Metropolitan Area (including The Woodlands, Sugar Land, Katy, and Pearland):
Houston is the Energy Capital of the World. Offshore operations, refinery hubs, and engineering firms require custom corporate apparel, moisture-wicking polo shirts, and flame-retardant (FR) blended work tees. Our cut and sew facility crafts heavy-duty work shirts featuring reinforced twin-needle stitching, anti-pilling synthetic knits, and heat-resistant reflective paneling engineered for Port of Houston logistics crews.
With the Texas Medical Center being the largest medical complex in the world, Houston scrub brands require high-performance technical fabrics. We manufacture antimicrobial, 4-way stretch poly-rayon-spandex scrubs and lab jackets engineered with fluid-barrier technology, ergonomic side paneling, and deep utility pocketing.
Houston’s vibrant music culture and streetwear scene demand heavy-gsm boxy fit tees (240 GSM to 300 GSM) and custom fleece hoodies (400+ GSM French Terry). Our cut and sew lines handle complex vintage acid washes, pigment dyeing, drop-shoulder silhouettes, and custom screen-printing or 3D puff embroidery with low 50-piece minimums.
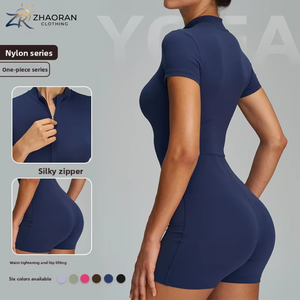
From local Houston run clubs to specialized badminton training facilities, performance activewear requires extreme ventilation. We engineer seamless nylon rompers, custom sublimated badminton team jerseys, and squat-proof compression leggings using interlock knit fabrics with moisture management indices exceeding 95% absorbency speed.
For growing Houston enterprises, transitioning from promotional blank printing to custom cut-and-sew garment engineering is a pivotal growth step. The table below outlines the structural technical advantages:
| Manufacturing Parameter | Standard Catalog Blanks | Custom Cut & Sew (Affix Apparel) |
|---|---|---|
| Fit & Pattern Customization | Fixed standard sizes (S-XL); limited boxy/oversized variations | 100% Custom Tech Pack pattern drafting & precision grading |
| Fabric Selection & GSM | Pre-selected inventory fabrics (typically 140-180 GSM) | Mill-direct custom GSM (120 to 500+ GSM), organic, OEKO-TEX knits |
| Seam Construction | Standard single/double needle lockstitch | Flatlock, 4-needle 6-thread, activewear safety stitch, taped seams |
| Dyeing & Color Matching | Basic stock colors | Pantone TCX/TPX exact lab-dip color matching & custom garment washes |
| Private Labeling Integration | Tear-away tags or neck relabeling over existing seams | Integrated woven main labels, satin care tags, size flags sewn in-line |
| Minimum Order Quantity (MOQ) | Low, but restricted design freedom | Low 50 Pcs per style with full custom design execution |
Houston apparel brands are restructuring their supply chains to combat extended overseas transit delays, high freight costs, and inventory overproduction. The current Texas apparel market is defined by three key trends:
Our turnkey manufacturing process ensures zero discrepancy between your original design vision and the final bulk shipment landed in Houston:
Our pattern engineers evaluate your sketches or physical samples to build a comprehensive tech pack specifying fabric weight (GSM), fiber content, seam allowances, artwork placement, and graded measurement charts.
We source raw fabrics from audited mills, perform lab-dip color matching against Pantone TCX codes, and execute shrinkage/color-fastness testing before bulk cutting.
A physical fit sample is manufactured in 7–12 working days. You test fit, drape, and stitch quality in Houston before granting final bulk production sign-off.
Computer-guided automated cutters ensure fabric piece accuracy. Screen printing (discharge, puff, water-based), embroidery, or sublimation are applied pre-assembly for seamless coverage.
Garments move through specialized stitching lines (flatlock, coverstitch, overlock) managed by experienced tailors, with constant inline seam-tension monitoring.
Every batch undergoes strict AQL 2.5 final inspection covering measurement tolerances, loose threads, packaging accuracy, barcoding, and direct dispatch to your Houston warehouse.
Combining North American design standards with scalable manufacturing efficiency to power growing apparel enterprises.
Launch custom collections without tying up capital in excessive inventory. Split 50 pieces across multiple sizes and colorways.
Access OEKO-TEX Standard 100 certified cottons, organic Pima cotton, and recycled polyester blends tailored for eco-conscious consumers.
Screen printing, 3D puff embroidery, DTG, discharge printing, and all-over sublimation executed under one manufacturing roof.
Custom woven main labels, printed neck tags, hangtags with barcodes, custom polybags, and retail packaging ready for store shelves.
Communicate directly with experienced apparel merchandisers who manage your production timeline from tech pack to cargo delivery.
Seamless logistics via air express (3-7 days) or ocean freight (25-35 days) directly to Houston, Austin, Dallas, and San Antonio hubs.
Essential guidance on custom cut and sew manufacturing, minimums, lead times, and logistics for Texas buyers.
Our standard MOQ starts at just 50 pieces per style. This can be split across a full size run (e.g., S to XL) and colorways depending on fabric availability. Highly engineered garments like raw denim or complex outerwear typically start at 100 pieces per style.
Sample development (pattern drafting, fabric sourcing, and proto sewing) takes approximately 7 to 12 working days. Once you approve the fit sample, bulk production for 50–500 pieces runs 15 to 25 working days. Express air freight to Houston adds 3 to 7 days.
Yes! Many of our Houston fashion founders come to us with physical sample garments, mood boards, or simple vector sketches. Our technical design team will translate your concept into a complete production-ready tech pack with full measurement grading.
For Texas humid weather, we recommend 100% combed ring-spun cotton (180–220 GSM) for breathable casual wear, bamboo-cotton blends for ultra-soft loungewear, and nylon-spandex micro-mesh with moisture-wicking finishes for sportswear and activewear.
Absolutely. We supply custom woven main neck labels, printed care/content labels compliant with US FTC regulations, branded cardboard hangtags, and frosted polybags with scannable UPC barcodes for immediate retail placement.
All production follows strict AQL 2.5 (Acceptable Quality Limit) standards. We inspect incoming raw fabrics, perform inline seaming audits during construction, and conduct a final 100% garment inspection for measurement compliance, thread trimmings, and print durability before sealing cartons.
Partner with an audited cut and sew clothing manufacturer trusted by startups, enterprise labels, and corporate buyers across Texas and worldwide.